Melting & refining
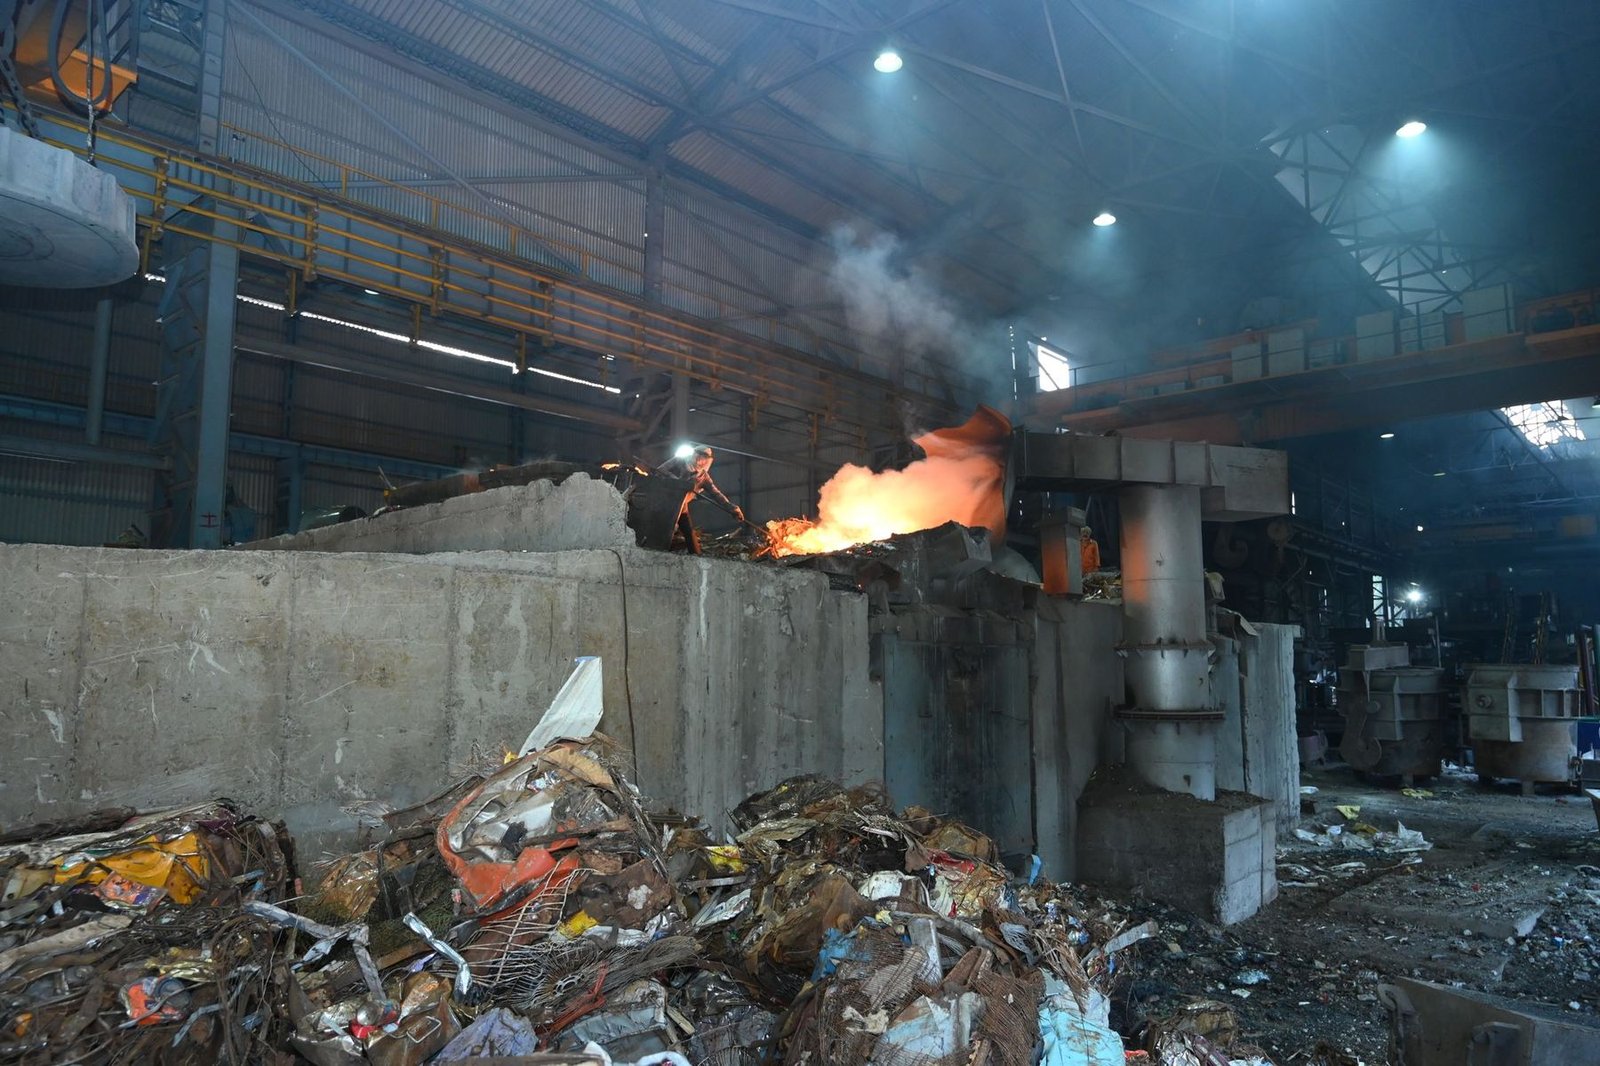
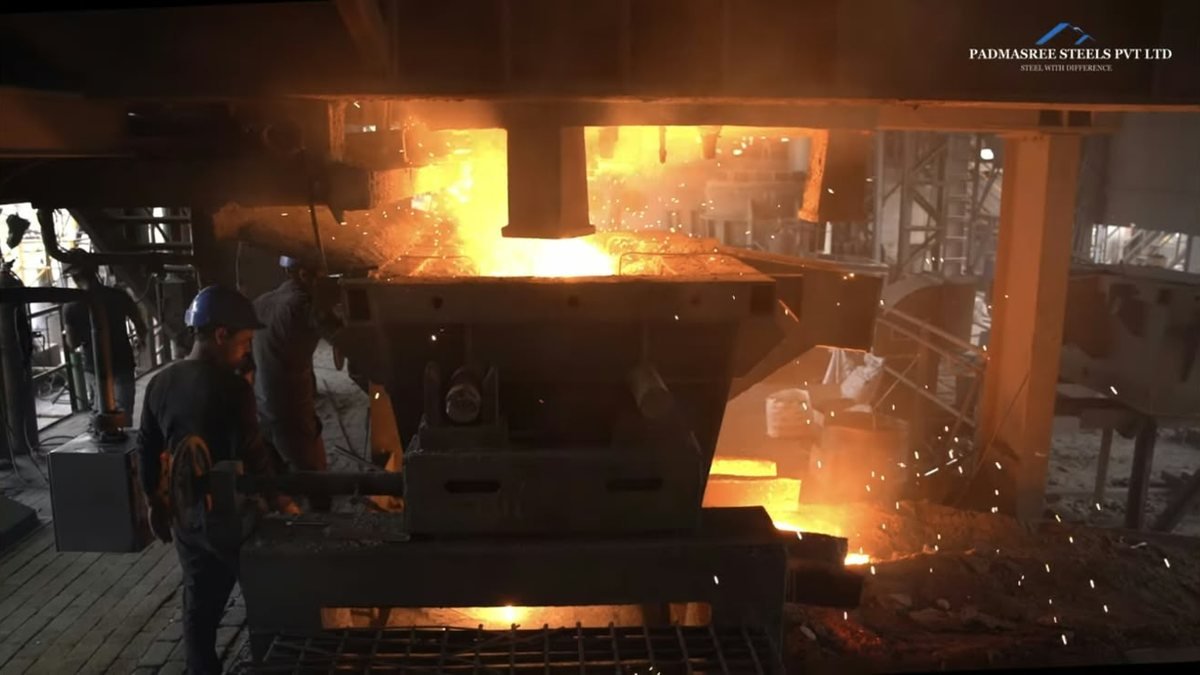
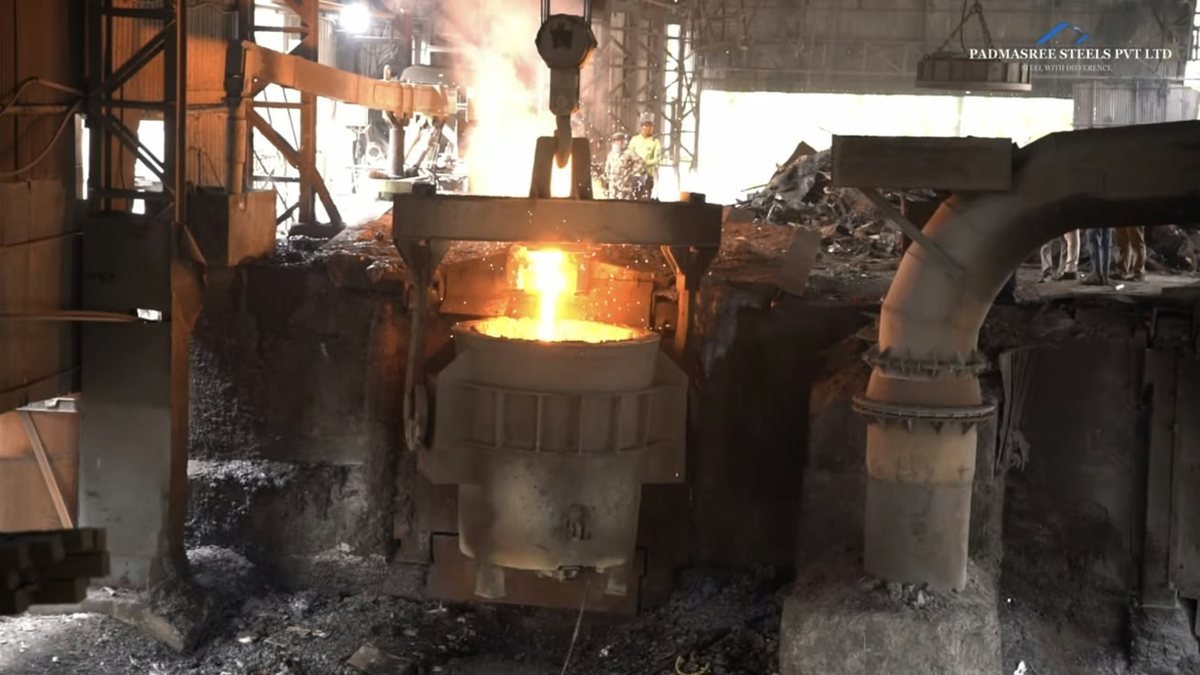
The raw material for our steel bars is processed in our in-house induction furnaces. Once melted, the molten metal is separated from the slag and purged in a ladle furnace to reach the desired chemical composition.
Micro-alloying materials are added and non-metallic inclusions are removed. Keeping the chemistry exact is crucial for weldability, ductility, strength and elongation, so we monitor it with a high-end spectrometer.
Continuous casting
Molten metal from the ladle refining furnace is poured through a tundish into a mould below, which casts a predetermined length of metal. New molten metal is supplied at a precise rate to keep up with solidification.
Our continuous casting machine improves yield, cost efficiency, productivity and quality.
Secondary cooling & hot charging
Billets leaving the casting machine enter a secondary cooling chamber, where they are sprayed with water for complete solidification. This keeps their shape and improves quality.
The billets are then reheated in our reheating furnace to recrystallise the metal, so it can be rolled without damaging the bonding.
Rolling mill
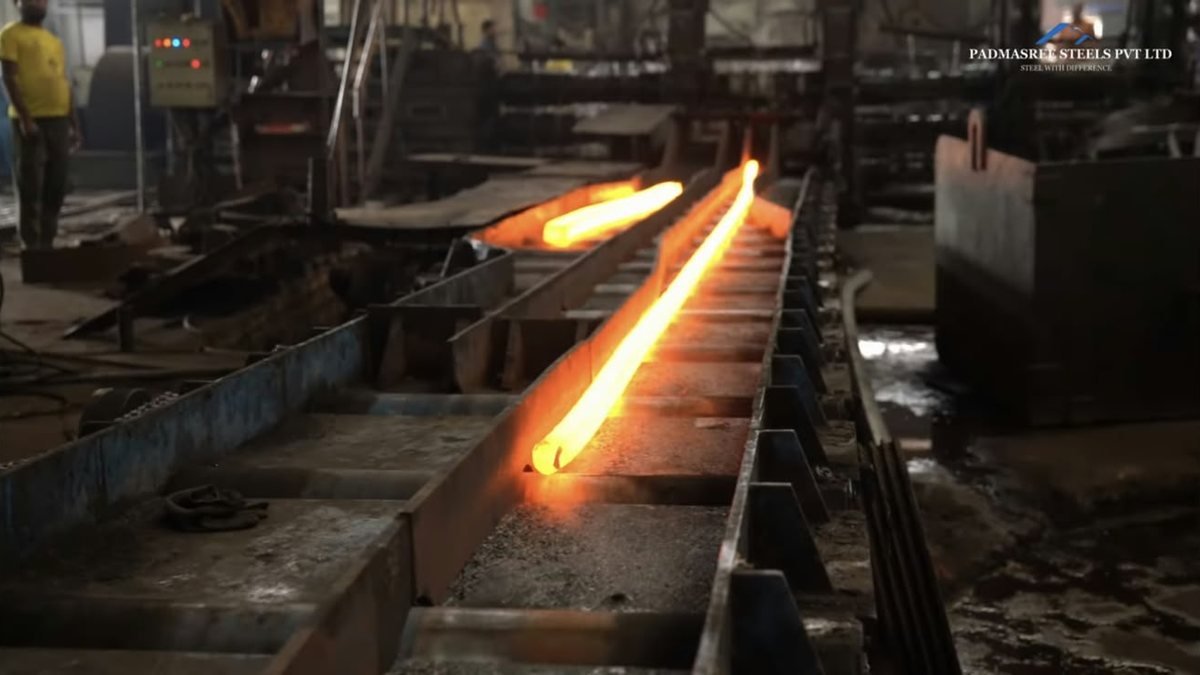
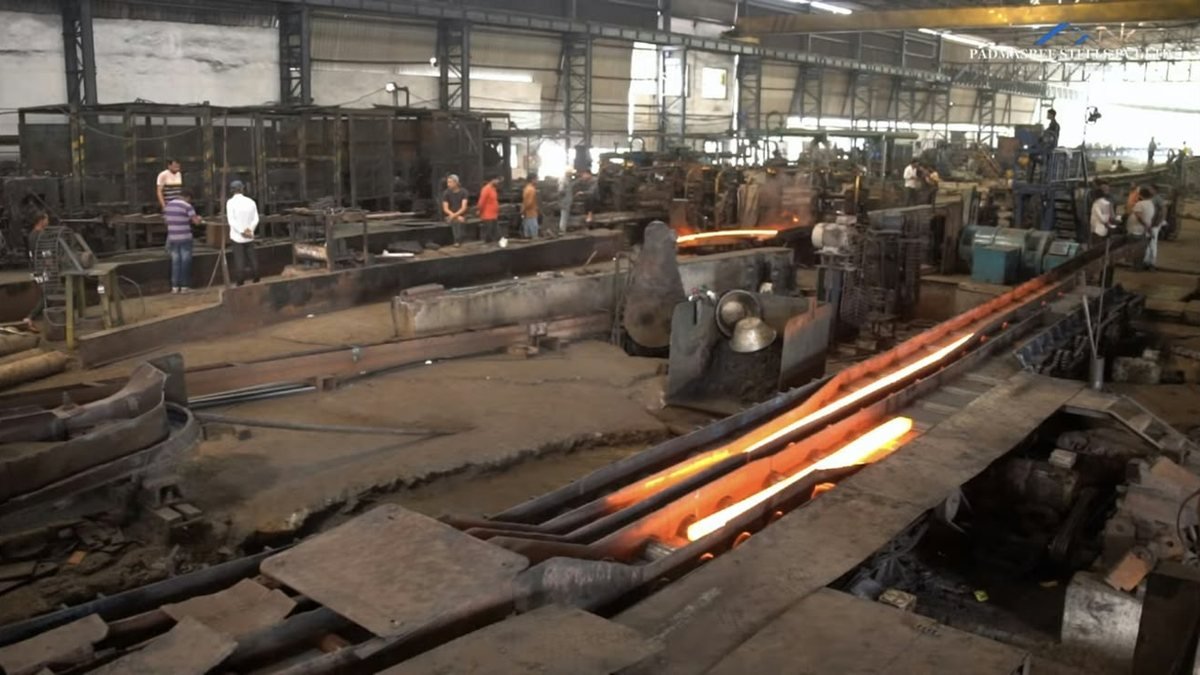
Billets travel by conveyor to the rolling mill, where the internationally accepted roll pass design gives higher strength and elongation. The fully automatic process keeps every bar uniform along its length.
The mill has a roughing mill of two 18″ stands, four intermediate mills, four pre-finishing mills and a finishing mill of six 12″ stands, each with its own DC motor for total automation.
Quenching & self-tempering
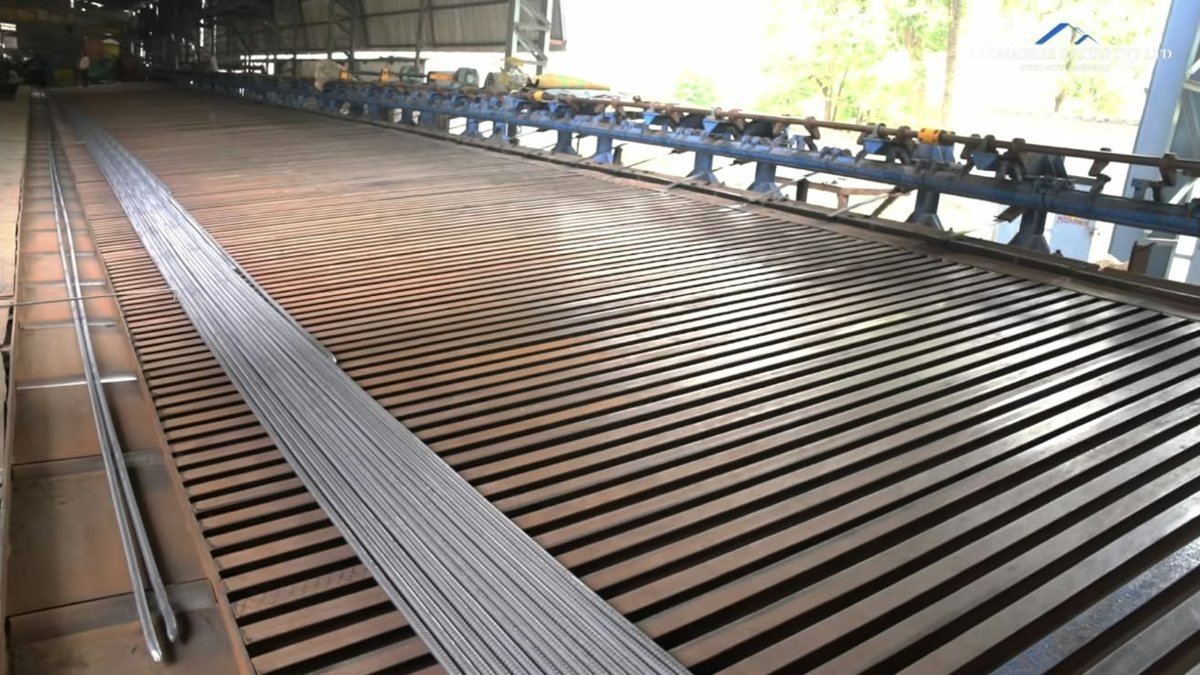
After the finishing mill, the bars pass through a water cooling chamber for quenching, in three stages: rapid cooling hardens the surface; the surface layer is then tempered by the heat left in the core; finally the bars cool in air on the cooling bed.
The result is greater strength, ductility, bendability and weldability in every bar.
Master bending
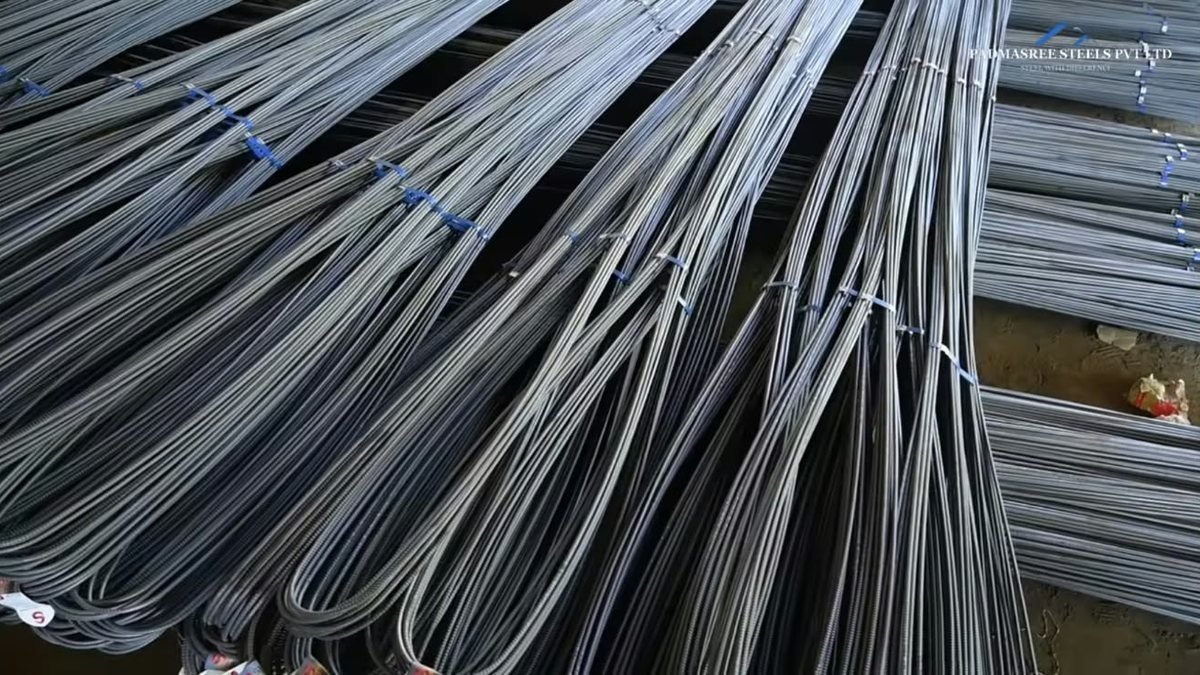
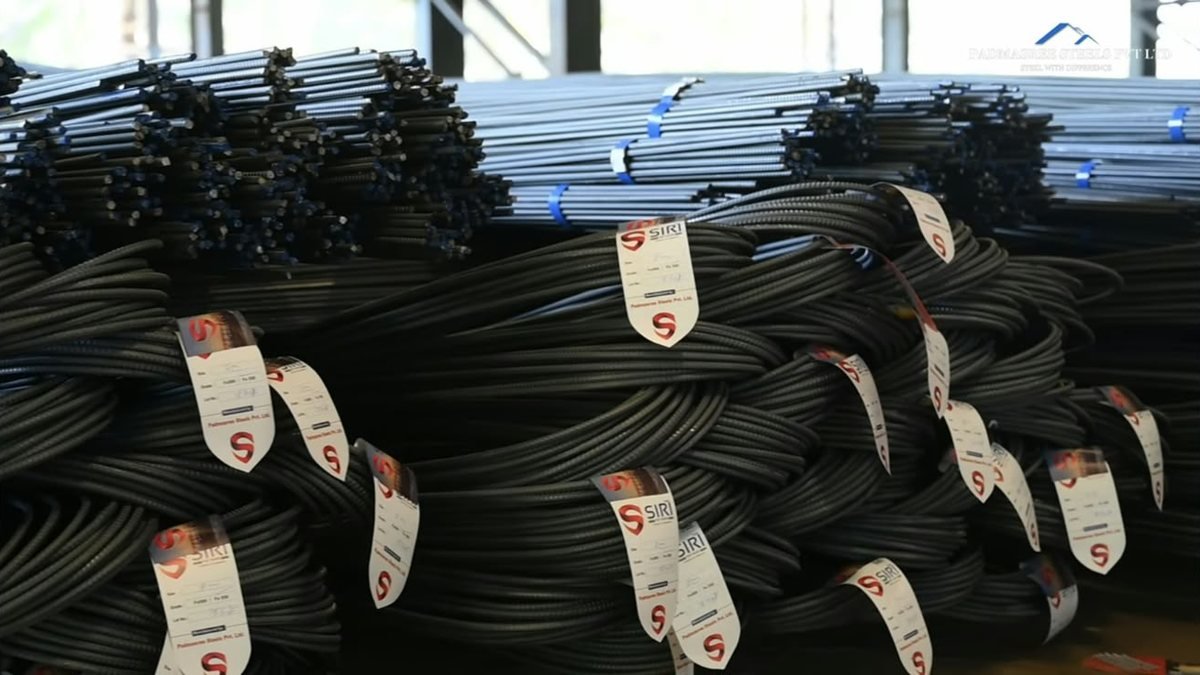
The finished TMT bars are master bent and neatly packed to the customer’s requirement.
Quality control lab
Samples are tested in our labs against the chemical composition and strength required by BIS for each grade. The sectional weight and strength of the bars are tested every 30 minutes.
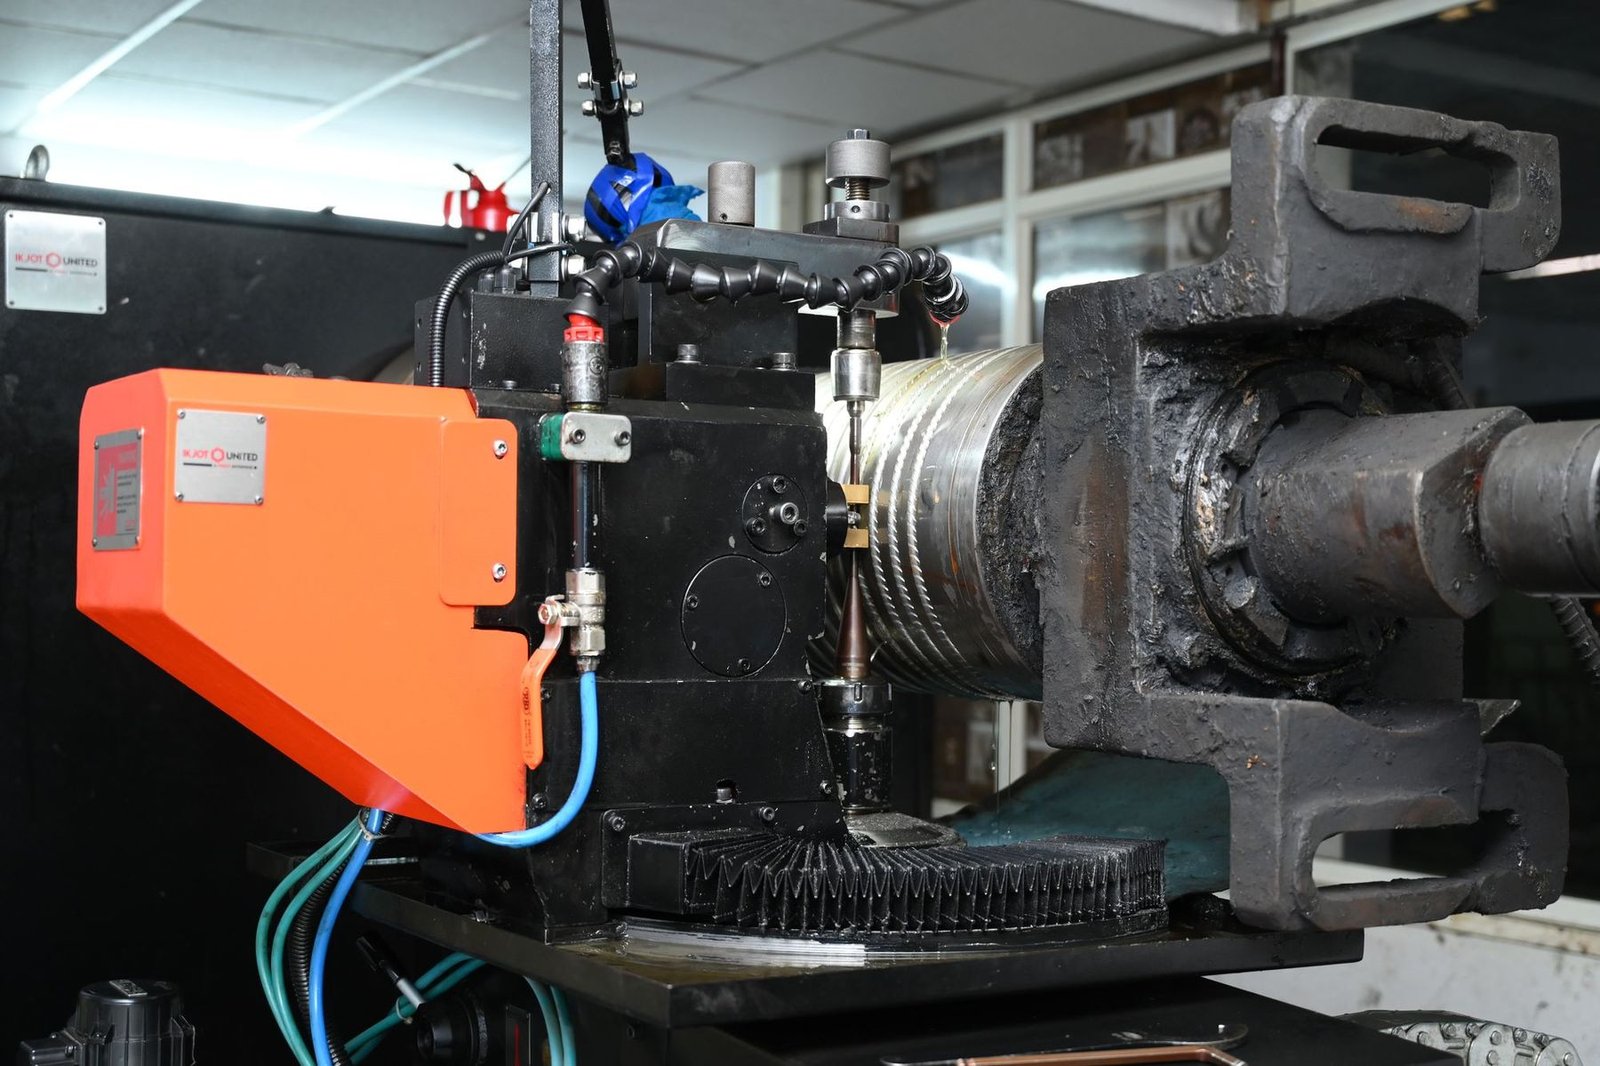
Computer-controlled notch-making machines engrave a precise, uniform, parallel rib pattern for excellent bond strength with concrete. The chemistry also supports easier welding without pre-heating.
Efficient transport pool
Delays in steel supply cost builders money. That is why we work closely with a large pool of reliable transporters, so material reaches your site on time.